Keeping Automatic Shrink Wrappers Running: A Maintenance Playbook
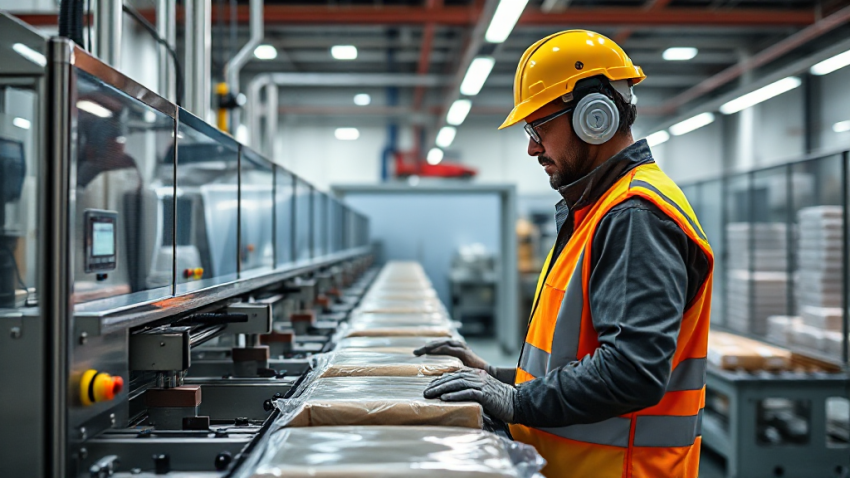
The line stops because a sealing bar has welded itself to a film web, and the operator is already reaching for a scraper. That scene repeats in plants that treat the wrapper as a black box until it fails. An Automatic Shrink Wrapping machine is a sequence of heat, pressure, motion and timing, and each element leaves a maintenance signature you can read before it becomes a stoppage.
This playbook is organized by component, because that is how failures actually appear on the floor. Each section pairs the symptom you will see with the routine that prevents it, and closes with a short daily and weekly block your team can own.
Sealing and Cutting Assembly: Where Most Stoppages Begin
The sealing bar is the hardest-working part of the wrapper. It cycles thousands of times per shift, carries a PTFE cover, and sits directly in the path of film tension. When it fails, the symptom is usually a weak seal, a curled edge, or film sticking to the bar and tearing on the next cycle.
Symptoms and the fix
- Smoked or brown seals: temperature set too high or dwell too long. Verify the thermocouple reading against a contact thermometer before adjusting the setpoint.
- Weak peel strength: pressure uneven along the bar, worn silicone pad, or a dull cutter leaving a ragged edge that opens under load.
- Film sticking to the bar: a torn or glazed PTFE cover. Replace it as soon as you see wrinkles or burn marks, not when it finally fails.
Check the sealing bar alignment weekly with a straight edge. A bar that is a fraction out of parallel produces seals that pass inspection on one side of the pack and fail on the other, which is far harder to diagnose later.
Shrink Tunnel: Airflow, Heaters and Conveyor Balance
Downstream of sealing, the shrink tunnel Machine is where film defects become visible. A tunnel that is drifting out of balance produces dog-ears, uneven shrink on one face, or film that sags at the trailing edge of the pack. None of these are film problems; they are tunnel problems.
Heater and airflow checks
Inspect heating elements for sag or discoloration during every planned stop. A single failed element in a multi-element bank creates a cold zone that shows up as a loose patch on the finished bundle. Clean the blower intakes and check that fan blades are free of film dust, because restricted airflow mimics a heater fault and sends teams chasing the wrong cause.
Conveyor and tunnel entry
Confirm the conveyor speed matches the seal cycle, and check that the tunnel curtain strips are intact. Missing or stiff curtains let heat escape at the entry, which forces operators to raise the tunnel temperature and over-shrinks the leading face. Replace curtain strips in sets, not one at a time.
Film Feed, Tension and the Wrapping Section
Film-related faults usually trace back to tension control rather than the film itself. A Shrink wrapping machine with a slipping brake or a worn dancer roller will produce loose wraps on some cycles and tight wraps on others, and the operator will blame the roll.
Common film-path mistakes
- Loading a roll without checking that the film passes on the correct side of every guide roller.
- Running a partially used roll until the core is exposed, which changes tension and causes tracking drift.
- Ignoring static buildup in dry conditions, which makes film cling to guides and misfeed at the sealing station.
Clean the film path with a dry, lint-free cloth at every shift change. Film dust accumulates on rollers and changes the friction that the tension system was set up against. Inspect the brake pad and dancer spring weekly, and log any adjustment so the next shift knows the baseline has moved.
Daily and Weekly Routine, Plus Spares That Prevent Repeat Stoppages
Most repeat stoppages come from a small set of consumables that were not on the shelf when they were needed. Build the routine around those parts and the machine will spend far more time producing than being repaired.
Daily routine before the first shift
- Wipe the sealing bar and confirm the PTFE cover is intact.
- Check film tracking through the guides and confirm the roll is seated squarely.
- Run two test packs and inspect the seal and shrink quality before releasing the line.
- Listen for unusual noise at the conveyor drive and blower during the first few cycles.
Weekly routine during planned downtime
- Inspect heaters, thermocouples and tunnel curtains.
- Check sealing bar alignment, pad condition and cutter sharpness.
- Clean blower intakes and confirm airflow is unobstructed.
- Verify brake and dancer tension against the recorded baseline.
Keep a spares kit with PTFE covers, silicone pads, cutter blades, thermocouples, curtain strips and fuses. A machine that waits two days for a cover is a machine that has already cost more than the part. Record every adjustment and replacement in a log tied to the machine, not to the shift, so patterns become visible over months rather than being rediscovered each time.
Maintenance on an automatic wrapper is not a repair activity; it is a production activity. The teams that treat the sealing bar, tunnel airflow and film path as scheduled items rarely see the jammed-bar stoppage that started this playbook, and when they do, they already know which component to check first.